
Most procurement decisions in the automotive supply chain are evaluated on price, lead time, and material certification. These are reasonable starting points, but they rarely capture the full cost of a poor vendor relationship. When a molder underdelivers — whether through dimensional inconsistency, poor tooling management, or communication breakdowns — the consequences ripple outward far beyond the rejected part. Rework, line stoppages, expedited freight, and engineering hours spent troubleshooting defective components add up quickly, often exceeding whatever was saved at the contract stage.
This is not a theoretical concern. It is a recurring pattern in U.S. manufacturing operations where sourcing decisions are made under time pressure, with too much weight placed on the initial quote and too little placed on operational fit. The goal of this guide is to help buyers, engineers, and operations managers understand what they are actually evaluating when they select a molder — and where the hidden costs tend to accumulate.
What Automotive Injection Molding Actually Demands From a Supplier
Automotive injection molding is a precision-driven process that operates under tighter tolerances and stricter quality expectations than most other industrial plastic forming applications. Components produced through this process — whether interior trim pieces, under-hood housings, fluid management parts, or structural clips — must perform reliably under mechanical stress, thermal cycling, and chemical exposure. The margin for variation is narrow, and the downstream consequences of a nonconforming part can affect vehicle safety, regulatory compliance, and brand reputation.
For buyers evaluating suppliers, a strong entry point is understanding how a molder positions itself within this space. Detailed service descriptions, such as those found under automotive injection molding offerings, can reveal whether a supplier has built genuine capability around automotive-grade requirements or is simply offering generic molding services with automotive clients on the side.
There is a meaningful difference between the two. A molder that has organized its operations around automotive quality standards will have documented control plans, mold maintenance schedules, and traceability systems already in place. One that has not will rely on reactive quality management — catching problems after they have already entered the supply chain.
The Tooling Relationship Is Often Underestimated
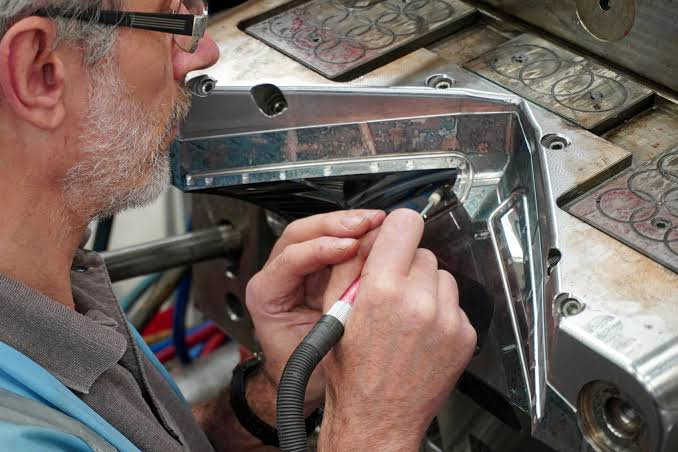
Tooling ownership and management is one of the least examined variables in supplier selection, yet it has significant long-term implications. When a buyer commissions a mold, they typically own that tooling. But the molder is responsible for maintaining it, storing it properly, and tracking its performance over time. A molder that lacks structured tooling management will allow shot counts to accumulate without scheduled maintenance, will store tools in conditions that accelerate wear, and will fail to document modifications made over the life of the mold.
When quality issues emerge months or years later, diagnosing the root cause becomes unnecessarily difficult. Was it a material change? A process drift? Tooling wear? Without documentation, each investigation starts from scratch. This is a hidden cost that rarely appears on any invoice but consumes engineering and quality team time consistently across the production relationship.
Process Control Is Not the Same as Quality Inspection
Many molders rely heavily on inspection at the end of the production run to catch defects. This is an older approach that creates waste regardless of the outcome — acceptable parts are shipped, defective parts are scrapped, and the root cause of the variation often goes unaddressed. In automotive supply contexts, this model is increasingly insufficient.
Process control means monitoring and adjusting variables during production — melt temperature, injection pressure, cooling time, cycle consistency — so that the process itself produces conforming parts rather than depending on inspection to filter out bad ones. Suppliers operating with this mindset will have documented process parameters, statistical process control records, and a clear escalation path when a process drifts outside acceptable limits. Buyers should ask to see this documentation rather than accepting general assurances.
Where Costs Accumulate Without Being Labeled as Such
The actual cost of a poor molder relationship is distributed across several functions that do not always communicate with each other. Quality teams absorb the inspection burden. Engineering teams absorb the troubleshooting time. Operations teams absorb the line disruption. Procurement absorbs the expediting cost. Because each cost is recorded in a different budget, the total rarely gets attributed to the original sourcing decision. This diffusion is one reason why underperforming supplier relationships persist longer than they should.
Qualification and Validation Time Is a Real Resource
Switching molders requires re-qualification of the process and re-validation of the parts. In regulated automotive supply environments, this can involve production part approval process documentation, dimensional studies, and material verification — all of which require engineering hours, lab testing, and customer approval. When a molder fails and must be replaced, this entire process restarts, consuming resources that were not budgeted for the transition.
The more embedded a molder is in a production program, the more expensive replacement becomes. This is why the cost of choosing incorrectly at the outset is often felt most acutely one to three years into a production relationship, when transitioning away has become logistically complex but performance has continued to decline.
Communication Gaps Compound Operational Problems
A technically capable molder that communicates poorly will still generate downstream costs. When a process change is made without notification, when a material substitution occurs without documentation, or when a production schedule change is not communicated in advance, the receiving plant is left managing consequences that could have been anticipated and planned for. These are not dramatic events. They are routine failures that accumulate quietly into a pattern of operational inefficiency.
Buyers should evaluate communication structure as deliberately as they evaluate technical capability. Who is the point of contact for quality issues? What is the response time expectation for non-conformance notifications? How are engineering changes communicated and approved? These questions reveal whether a molder has built an account management structure that supports long-term program stability or whether communication is informal and reactive.
Evaluating U.S.-Based Molders in the Current Supply Environment
Domestic sourcing decisions in the automotive sector are increasingly influenced by supply chain resilience considerations that did not carry the same weight five years ago. Extended lead times from offshore suppliers, freight volatility, and the difficulty of managing quality issues remotely have prompted many OEMs and Tier 1 suppliers to reassess how much of their molded component volume should be produced domestically. This shift has increased demand for qualified U.S.-based molders and, in some cases, has outpaced available capacity among suppliers with the right capability profile.
Capacity and Scheduling Transparency Matter More Than Proximity
Selecting a U.S.-based molder primarily for geographic proximity without evaluating capacity commitments is a common oversight. A molder running at high utilization may not have the scheduling flexibility to accommodate design changes, rush orders, or production increases without pushing back on other programs. Understanding a molder’s current capacity picture — how much of their press time is committed, how they prioritize programs when conflicts arise, and what their lead time looks like under normal versus peak demand — is relevant to assessing whether they can actually serve a program well over its full life.
Certification Status Reflects Operational Maturity
Quality management certifications in the automotive sector, such as IATF 16949, reflect a molder’s commitment to structured quality systems rather than ad hoc quality management. As described by the International Automotive Task Force, this standard defines requirements for quality management systems within the automotive production supply chain and is a meaningful signal of operational maturity. A molder that has achieved and maintained this certification has demonstrated that its processes, documentation, and corrective action systems meet a recognized industry benchmark.
That said, certification alone does not guarantee performance. It is a baseline, not a guarantee. Buyers should review audit findings, corrective action histories, and customer references to understand how a certified molder actually performs under the pressures of real production programs.
What a Rigorous Supplier Evaluation Actually Looks Like
Effective supplier evaluation for automotive injection molding goes beyond a site visit and a capability statement. It involves asking specific questions about how the molder manages known failure points — tooling wear, process drift, material traceability, non-conformance handling — and what their documented response is when these issues arise.
Useful evaluation areas include:
• How the molder documents and tracks tooling condition, including maintenance intervals and modification history, across multi-year programs.
• Whether the molder operates with real-time process monitoring or depends on end-of-run inspection to identify quality problems.
• How non-conformances are logged, communicated to the customer, and resolved with documented corrective actions that prevent recurrence.
• What the molder’s policy is on material substitutions, and how those changes are approved and documented before production continues.
• How scheduling conflicts are handled when multiple programs are running simultaneously and capacity becomes constrained.
These questions do not produce definitive answers on their own, but the specificity and confidence with which a molder responds tells a buyer a great deal about whether operational discipline is embedded in their culture or is simply performed during evaluation.
Conclusion: The Real Selection Criterion Is Operational Fit
Choosing an automotive injection molder is not primarily a purchasing decision — it is an operational partnership decision that will affect quality outcomes, engineering workload, and production stability for the duration of a program. The buyer who selects based on price and delivery lead time alone is optimizing for the contract stage while accepting risk across every subsequent stage of the relationship.
The hidden costs discussed throughout this guide — tooling degradation, process drift, communication failures, re-qualification burden — are not unpredictable. They are the predictable outcomes of misaligned supplier selection. A molder with the right technical capability, the right quality systems, and the right communication structure will reduce these costs not by eliminating complexity, but by managing it consistently before it becomes a problem.
The investment in a thorough, structured evaluation process at the outset is almost always smaller than the cost of managing a failing supplier relationship in the middle of active production. U.S. buyers who treat this selection as the operational decision it actually is will make better choices — and will be better positioned to hold their suppliers accountable when performance matters most.
